If you’ve ever stood next to a hand pallet truck in a warehouse, loading dock, or small retail storeroom, you might have dismissed it as a simple, unassuming tool—just a metal frame, two forks, and a hydraulic pump that lets you heft heavy pallets. But after 12 years as a hand pallet truck supplier, I’ve learned that the unsung workhorse of material handling is far more than that. The most important part of any good hand pallet truck isn’t just its lifting capacity or build quality: it’s the safety features built into its design, ones that prevent bruises, broken bones, and even serious accidents in busy workplaces. Today, I want to walk through the safety features I’ve helped test, refine, and recommend to my customers over the years, because too many operators (and even some business owners) don’t realize how much protection is packed into that small, maneuverable machine. Hand Pallet Trucks
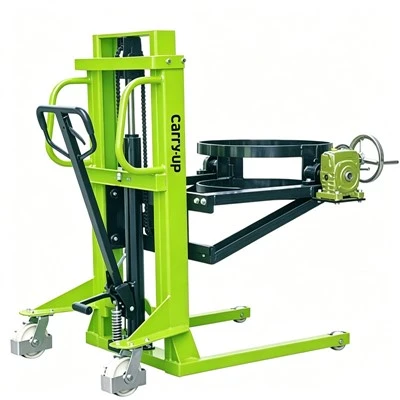
Let’s start with the most basic, and often most misunderstood, feature: the load backrest. You’ve seen them—those solid metal bars that extend up from the back of the forks, just below the handle. At first glance, it looks like a simple guard, but its purpose is far more critical than just keeping boxes from falling. Last year, I worked with a small grocery distributor that told me their operators were always trying to skip attaching the backrest, saying it slowed them down. Within three months, they reported two separate incidents: one where a 50-pound bag of grain fell off a pallet and hit an operator’s foot, fracturing a toe, and another where a stack of canned goods toppled backward onto a pallet that was being turned around a tight aisle, narrowly missing a worker’s head. After we worked with them to train their team on why the backrest matters, they started requiring it for every lift—and in the year since, they haven’t had a single similar incident. The backrest isn’t there to slow you down; it’s there to stop loose or shifting loads from falling, especially when you turn, brake, or navigate uneven surfaces. Good backrests aren’t just thin sheet metal, either: the ones my team supplies are reinforced at the corners and made from high-tensile steel, so they don’t bend or crack if a load accidentally hits a wall or another piece of equipment.
Next up is the handbrake system, and this is a feature that separates budget models from the ones that will keep operators safe in icy loading docks, sloped driveways, or tight parking lots. Many cheap hand pallet trucks have a basic brake that only stops the wheels when you’re going forward, but the reliable ones we carry have a dual-action foot brake. That means you can press down on the pedal to slow or stop the truck when you’re moving forward, and if you need to hold a load on an incline, you can engage the secondary, locked position with a push of your heel. Last winter, a manufacturing client in a city with frequent ice storms told me they’d had three trucks slip backward down their loading ramp in the past two years, all because their old hand pallet trucks had brakes that couldn’t hold on even a 2-degree slope. We swapped those out for our trucks with the dual-action brake, and they’ve only reported one near-miss since—an operator stepped off the truck quickly, and the brake held the load in place without moving an inch. The other brake feature worth noting is the emergency stop handle, built into the top of the truck’s operating lever. If an operator’s clothing gets caught on a pallet, a wall, or another truck mid-move, they can push the emergency stop to cut power to the hydraulic system and lock the wheels, stopping the truck instantly before they get dragged or crushed. It’s a small lever, but it’s one of the first things I point out to new operators during training.
Hydraulic system safety is another area that’s often overlooked, but it’s where most hand pallet truck-related injuries happen. If you’ve ever had a pallet truck’s hydraulic cylinder leak fluid mid-lift, or suddenly drop a heavy load when you’re halfway across a dock, you know how dangerous that can be. That’s why all the hydraulic pumps I supply have a pressure relief valve, calibrated to shut off automatically if you try to lift a load heavier than the truck’s rated capacity. I’ve seen operators try to cram a 5,000-pound load onto a truck rated for 4,500 pounds just to save a trip—and every time, the pressure relief valve activates, stopping the lift before the truck can tip or the hydraulic lines burst. That valve isn’t just a convenience; it’s a fail-safe. We also use sealed hydraulic systems on all our trucks, so dirt, dust, and warehouse debris can’t get into the lines and cause a leak. Leaks on the warehouse floor aren’t just messy, either—they create a slip hazard that can lead to falls. A few years ago, we had a client in a distribution center that switched to cheap, open hydraulic hand pallet trucks, and in six months, they had seven slip injuries from leaked hydraulic fluid on their concrete floors. Switching to our sealed systems not only eliminated those leaks but also cut their slip-related incidents by 85% in the next quarter.
Ergonomic safety features are just as important as mechanical ones, because the biggest risk with hand pallet trucks isn’t a catastrophic accident—it’s the cumulative wear and tear that leads to chronic pain and long-term injuries. The handle on a hand pallet truck isn’t just for steering; good handles are padded with non-slip, ergonomic grips that reduce strain on an operator’s wrists and forearms during long shifts. I’ve used a lot of budget trucks where the handle is hard plastic, and after 20 minutes of pushing, my hands start to ache. The ones we supply have grips that curve to fit the natural shape of the hand, so operators don’t have to grip too tight, even when they’re pushing heavy loads down a long aisle. Another ergonomic feature is the handle’s adjustable height. Operators of different heights often have to hunch or stretch to reach a standard handle, leading to back strain. Our trucks let you adjust the handle in 2-inch increments, so a 5’2” stock clerk and a 6’2” warehouse manager can both use the same truck comfortably, without straining their spines. Even the wheels matter here: we use dual front wheels on all our hand pallet trucks, not single wheels, which distribute the weight of the load more evenly and make turning and navigating uneven surfaces (like cracked concrete or small ramps) much easier. Single front wheels can catch on uneven surfaces, causing the truck to tip or jerk suddenly, which is a top cause of operator falls.
Last, but certainly not least, is load stability and visibility features. Good hand pallet trucks are designed with a low center of gravity, so even when lifting a full, heavy pallet, they don’t tip over when going around a corner or stopping suddenly. Some models, including the ones my team supplies, have a load sensor indicator: a small light on the handle that turns red if the load is too far to one side, alerting the operator before they try to turn. Visibility is also key: many operators stack pallets high, so they can’t see over the load when they’re moving, which can lead to collisions with other trucks, racks, or people. We offer optional side mirrors for hand pallet trucks that attach to the forks, so operators can see around tall loads without having to walk backward, which is a huge safety win in crowded warehouses. I remember a small retail chain that added these mirrors to all their trucks after a part-time operator backed into a display of glass jars, breaking $1,200 worth of inventory and cutting their shift short for a week. Six months later, they told me they hadn’t had a single collision with another truck or display since.
Now, I know what some of you are thinking: “This sounds like a lot of features, and all these extras must make the truck way more expensive.” I won’t lie—cutting corners on safety will save you a little money upfront, but it will cost you way more in the long run. We’ve had customers come to us after buying cheap hand pallet trucks for $300 less per unit, only to pay for two or three workers’ compensation claims, replacement damaged inventory, and downtime when their main truck was out of commission for repairs. The hand pallet trucks I supply are built to last 10 years or more, and their safety features aren’t add-ons—they’re part of the core design that keeps your team working safely and your operation running smoothly.
If you’re shopping for hand pallet trucks for your warehouse, retail space, or manufacturing facility, don’t just look at lifting capacity or price. Ask about the load backrest, dual-action brakes, pressure relief valves, ergonomic handles, and stability features. These aren’t just buzzwords—they’re the features that will prevent injuries, reduce damage, and save you money over time.
If you’re ready to replace your current fleet or upgrade to safer, more reliable hand pallet trucks, I’d be happy to walk you through our models, answer questions about safety features specific to your workspace, and help you find the right fit for your team and budget. Reach out to me today to start the conversation about what you need, and let’s make your material handling operations safer together.
Hand Pallet Trucks References
American National Standards Institute (ANSI). (2020). Safety Standard for Powered Industrial Trucks. ANSI/ITSDF B56.1-2020.
Occupational Safety and Health Administration (OSHA). (2022). Material Handling: Hand Trucks and Pallet Jacks. OSHA 3247-10.
Material Handling Industry (MHI). (2021). Best Practices for Hand Pallet Truck Safety in Warehousing and Distribution Centers. MHI Technical Report Series.
Hangzhou Carry Equipment Co., Ltd.
Hangzhou Carry Equipment Co., Ltd. is one of the most professional hand pallet trucks manufacturers and suppliers in China, also supports customized service. Please feel free to buy advanced hand pallet trucks for sale here and get quotation from our factory. For price consultation, contact us.
Address: No.360 Tongxiang Rd., Yinzhou Economic Development Zone, Yinzhou Dist., Ningbo, China
E-mail: Sales@carryupmhe.com
WebSite: https://www.carrymhe.com/
